Combed vs Carded vs Open-End Yarn: Differences and Uses by Product
Combed and carded yarn differ in fiber preparation; ring and open-end yarn differ in how they are spun. Property tables, product examples with sources and how to write yarn into a quote.
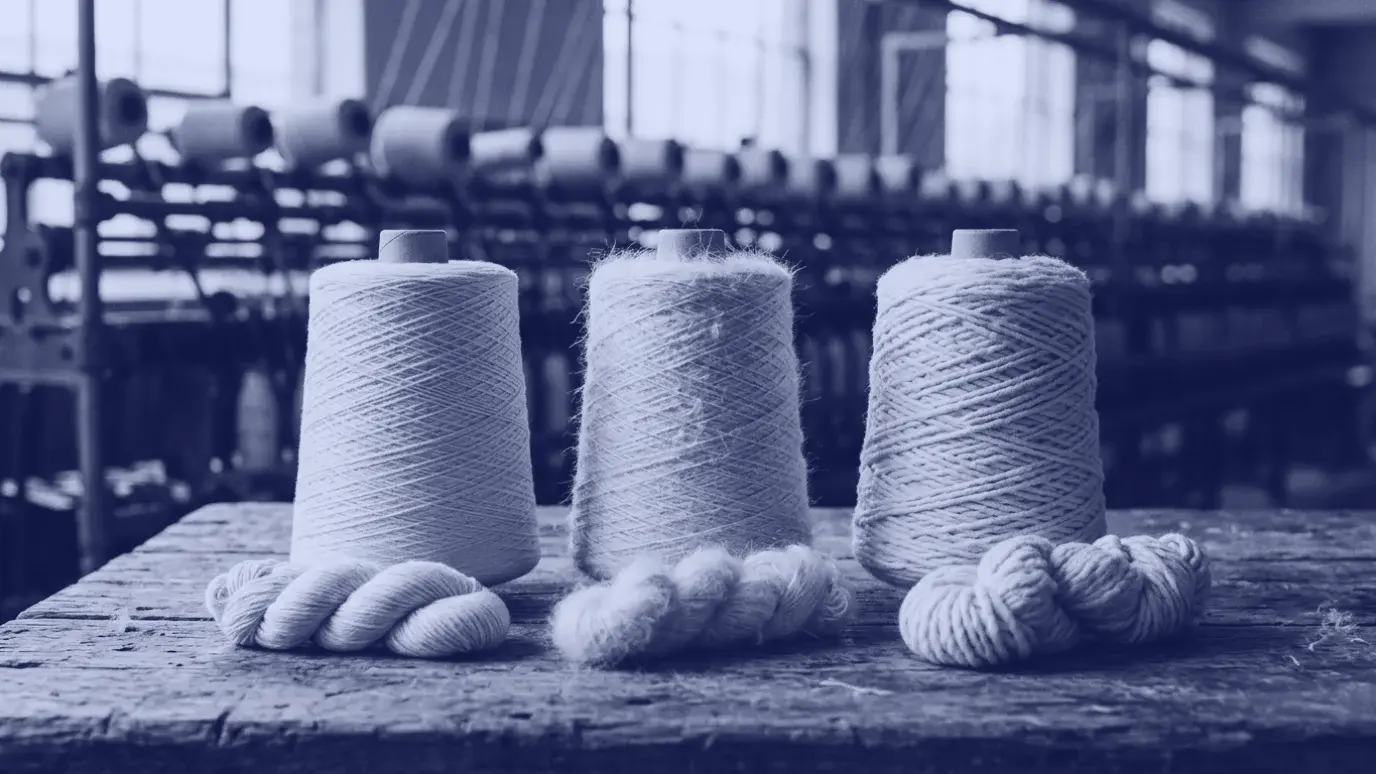
- Published:
- Updated:
- Fact-checked by:
- Gizem Polat
Key facts
- Combed and carded describe whether cotton is combed before spinning; ring and open-end describe how the yarn is spun, so the three cannot be compared on one axis.
- Combing removes short fibers, neps and trash; combed yarn is more even, softer and less hairy but costs more than carded yarn because of the extra step and waste.
- According to Cotton Incorporated, open-end yarn is 10–30% weaker than ring yarn spun from the same fiber, but more even, less hairy and cheaper.
- Open-end is economical at roughly Ne 1–40; ring yarn made from long fiber can go far above Ne 100 (Cotton Incorporated).
- Writing only “combed” (penye) on a quote is not enough: fiber preparation, spinning system, count and combing level must be written separately.
The difference between combed and carded yarn is whether the cotton is combed before spinning: combed yarn (penye in Turkish) is spun from combed cotton, carded yarn (karde) from uncombed cotton. Open-end and ring answer a different question: how the yarn is twisted and spun. The three therefore cannot be compared in one row; a yarn can be both carded and open-end, or both combed and ring-spun (Cotton Incorporated, ISP 1006).
This guide separates the two axes, shows the combed–carded and ring–open-end differences in tables, gives sourced examples by product and explains how to write the yarn type on a quote. Short definitions of the terms are in the glossary; this page is about comparison and choice. For count conversions, see the yarn count conversion guide.
Combed, carded and open-end yarn are not on the same axis
According to Cotton Incorporated, cotton yarns are often classified by spinning system: ring, open-end and air-jet (vortex included). Fiber preparation differs somewhat between these systems (ISP 1006). Carding is part of all of them; all cotton and cotton-blend fibers, including those that go into combed yarn, pass through the card first (Cotton Incorporated, Textile Yarns). Combing is a step added after carding. The roving step belongs to ring yarn only; open-end spins directly from sliver.
The two questions are independent:
| Carded (uncombed) | Combed (penye) | |
|---|---|---|
| Ring | Carded ring yarn | Combed ring yarn: fine counts are often spun on this line |
| Open-end (rotor) | Standard open-end yarn: there is no combing step in the flow | Not in the standard flow but possible: rotor spinning with combed sliver has been studied |
Source: Cotton Incorporated, ISP 1006 (process flow table) and Textile Yarns; Rowe (1993).
Combed and open-end are not mutually exclusive. Rowe (1993) describes how rotor yarn quality can be raised with combed cotton sliver; Cotton Incorporated, after giving the economical count range of open-end, adds that finer counts need combing to be spun without defects and weakness (Textile Yarns). There is a link in the other direction too: in Rieter's 2020 study, the waste of the combing line (comber noil) was tried as a raw material for rotor spinning in blend ratios from 0% to 100%; in Rieter's denim weft example the raw material is 70% cotton and 30% noil.
In everyday Turkish trade talk, penye also names a knit fabric; in this guide it is used only for yarn. You may meet two more variants on a quote: compact ring, where a suction unit added to the ring frame makes the yarn tighter, less hairy and stronger; and vortex, a newer type of air-jet spinning that gives a ring-like look and can spin 100% cotton (ISP 1006; Textile Yarns).
| Turkish term on a quote | English term |
|---|---|
| penye iplik | combed yarn |
| karde iplik | carded yarn |
| ring iplik | ring-spun yarn |
| open-end (rotor) iplik | open-end (rotor-spun) yarn |
| penye telefi | comber noil (waste removed by combing) |
Combed vs carded yarn: what does combing change?
Combing removes short fibers, neps and remaining small trash from the sliver that comes off the card, and makes the fibers more parallel; the waste removed is called comber noil (ISP 1006). According to Cotton Incorporated the waste share is 4% to 24%; according to NPTEL (IIT Delhi) it is 8% to 25%, depending on the industry and requirement. Cotton Incorporated's comparison for ring yarn is as follows:
| Property | Carded ring yarn | Combed ring yarn |
|---|---|---|
| Fiber length | Shorter | Longer |
| Evenness | Less even | More even |
| Neps and trash | More | Less |
| Fiber parallelism | Less | More |
| Strength | Lower | Higher |
| Count range | Coarser | Finer |
| Surface | Hairier | Smoother |
| Luster | Less | More |
| Processing cost | Lower | Higher |
Source: Cotton Incorporated, Textile Yarns, p. 11. The table shows direction, not the size of the difference; the source gives no numerical values.
Two consequences of combing stand out in practice. The first is twist: because the fibers are longer, combed yarn reaches similar strength with less twist than carded yarn; that means a softer yarn and fabric and less torque (tendency to twist out of shape). Combed yarn also tends to pill and shed fibers less (Textile Yarns; ISP 1006). The second is the combing level: quality depends on the share of noil removed and on whether the yarn is fully or partly combed. Partly combed yarn is made from a blend of combed and uncombed sliver; for the same input quality, a line that removes 16% noil gives a better yarn than one that removes 10% (Textile Yarns). That is why writing only “combed” on a quote is incomplete information.
Combed is not always necessary or “better”, either. According to NPTEL, in coarse and medium counts combing is an optional process to raise the yarn's cleanliness, smoothness and strength; in fine counts it is essential. The extra process, the waste and the intermittent operation make combed cotton more expensive than carded cotton. The sources do not give the size of the price gap; for a comparison, get written quotes for the same count and the same preparation level.
Open-end vs ring yarn: the spinning-system difference
In ring spinning, fibers leave the drafting system as a continuous, ribbon-like strand and twist is inserted in the yarn. In open-end spinning, fibers are separated one by one from the sliver, collect in the groove of a fast-spinning rotor and are twisted there. Cotton Incorporated sums it up this way: ring yarn forms from the outside in, open-end yarn from the inside out (TRI 1004). In the rotor, some fibers wrap around the yarn instead of being twisted into it; these wrapper fibers do not add to strength and are specific to open-end yarn (ISP 1006).
| Criterion | Ring yarn | Open-end (rotor) yarn |
|---|---|---|
| Strength | Strongest yarn | 10–30% weaker with the same fiber (TRI 1004); 15–20% in general (Textile Yarns) |
| Evenness and defects | Less even | More even, fewer yarn imperfections |
| Hairiness | Hairier; up to 90% of fiber ends can protrude from the surface | Less hairy; usually 25% or fewer of the fiber ends are on the surface (TRI 1004) |
| Handle | Softest | Harder (wrapper fibers) |
| Torque | More | Less |
| Bulk | – | At the same count the diameter is slightly larger and the yarn bulkier (TRI 1004) |
| Count range | From Ne 1; with long fiber far above Ne 100 | Economical at Ne 1–40; finer counts need combing |
| Productivity and cost | Lowest productivity, most expensive | Productivity per position 8–10 times higher, fewer process steps, cheaper |
| Twist direction | Z and S | Z only |
Source: Cotton Incorporated, ISP 1006 (p. 7), Textile Yarns (pp. 15–16, 20–21) and TRI 1004 (pp. 9–10).
These figures come from bulletins published around 2003 and 2010 and show the general trend. The gap depends on fiber length: according to TRI 1004, with fibers longer than 1-1/8 inch (about 28.6 mm) open-end yarn can be up to 25–30% weaker than ring yarn; as fiber gets shorter the gap shrinks quickly, and at some coarse counts open-end can even be slightly stronger. Open-end tolerates short fibers better; the ring drafting system needs a minimum fiber length to control the fibers (TRI 1004). The handle of open-end yarn also changes with setup: according to ISP 1006, if a more abrasive navel (the part at the yarn exit) is chosen, the yarn becomes softer and bulkier.
In fabric: strength, pilling and abrasion
A yarn difference does not carry into fabric in one direction. Candan and colleagues (2000) compared ring and open-end cotton yarns in plain jersey and lacoste knit fabrics (the abstract's term): fabrics made from open-end yarn had lower bursting strength and more pilling, and ring was slightly better in abrasion resistance. Hailemariam and Muhammed (2024) reported, for 3/1 twill denim woven from Ne 10 cotton yarn, that the ring-yarn fabric was better in tensile and tear strength, and the rotor-yarn fabric in abrasion resistance, pilling resistance and air permeability.
On pilling, the two studies point in opposite directions (ring better in knits, rotor better in woven denim); the fabric type, count and date of the work differ. No general statement such as “open-end always pills more” or the reverse can therefore be made. For a firm decision, knit the target fabric from each yarn and compare them with the same test.
Company directory
Looking for manufacturers in this field?
Browse companies in the related categories or get quotes from several companies with one form.
Do you manufacture or offer services in this field?
Which yarn for which product? Sourced examples
The sources give no binding table matching products and counts. The rows below summarize examples from the sources; the Rieter rows are brochure examples from a machine maker, not a market standard.
| Use | Yarn | Basis in the source |
|---|---|---|
| Lightweight fabrics | Ring yarn; fine counts are often spun from combed cotton | Cotton Incorporated: lightweight fabrics typically contain ring yarn because the spinning limit of open-end is at coarser counts (Textile Yarns); fine counts are often spun from combed cotton (ISP 1006) |
| T-shirts and sweatshirts | Open-end examples exist | Cotton Incorporated: open-end yarn is used in underwear, socks, sweaters, denim and outerwear (Textile Yarns). Rieter examples: T-shirt Ne 20–30 in 100% cotton, sweatshirt Ne 18–20 |
| Denim | Both ring and open-end yarn are used | Rieter weft example Ne 16 (70% cotton, 30% noil); in Ne 10 denim, ring was better in tensile and tear strength, rotor in abrasion and pilling (Hailemariam and Muhammed, 2024) |
| Towels | The specification decides | The Bursa Towel (Bursa Havlusu) geographical indication requires at least Ne 20/2 ring yarn (490–520 turns/m) in the ground warp and does not allow open-end (TÜRKPATENT, registration no. 1519, January 9, 2024); Rieter, on the other hand, gives a Ne 17 rotor example for a towel ground warp |
The last row matters: sometimes the yarn type is not a technical preference but a written obligation. As of October 11, 2026, the Bursa Towel rules are in the geographical indication registration text at TÜRKPATENT. If you produce under this indication or a customer specification, check the current text, and if needed consult the registering body (Bursa Ticaret Borsası, the Bursa commodity exchange) or an expert. How to read this decision in towel yarn is covered in terry towel quality; the choice among single jersey, piqué, interlock and rib for T-shirts is covered in T-shirt fabric types. Tekstil Rehberi's starting point is this: if a fine, soft handle is the priority, start with combed ring; if cost and an even surface are the priority, also ask for carded and open-end quotes, and compare the samples with the same test.
How common is open-end spinning in Turkey?
According to ITMF's estimate for the end of 2023, Turkey has about 8.80 million short-staple (ring) spindles, 948,550 rotors and 57,380 air-jet spindles installed; the world total is 231.7 million spindles and 9.71 million rotors (ITMF, International Textile Industry Statistics 66/2023). From these, Turkey holds about 3.8% of the world's spindles and about 9.8% of its rotors; the ratios are Tekstil Rehberi's calculation. Because the productivity of one rotor position is 8–10 times that of a ring spindle (ISP 1006), these ratios are not production shares; ITMF's table does not separate combing lines or yarn counts either. According to ITMF's 2022 shipment data, Turkey, together with China and India, was among the world's three largest rotor investors; Turkey's rotor investment had risen 91% over the previous year (Textile World, June 2023).
How to write the yarn type on a quote or spec
Saying “combed yarn” or “open-end yarn” alone is not enough. The order below is a starting point for writing the different axes separately:
- Fiber and composition: 100% cotton, cotton-polyester and so on, in percentages.
- Fiber preparation: carded or combed (penye). For combed, ask whether it is fully or partly combed and the combing level (the percentage of noil removed).
- Spinning system: ring, compact ring, open-end or vortex.
- Count and ply: with the name of the system, for example Ne 30/1. Use the yarn count converter if you need to convert.
- Twist direction: ring yarn can be Z or S twist; open-end is Z twist only (Cotton Incorporated).
- Quality values: evenness (CVm), yarn imperfections, hairiness and strength. In Uster Statistics the curves are separate by yarn type and count (Rieter, Figure 1); compare reports only for the same type and the same count.
Example line: “100% cotton, Ne 30/1, fully combed (penye) ring yarn, with an evenness, imperfection and hairiness report.” This information may not appear on the product label; ask the supplier in writing. If you need measurements, you can find firms in the textile testing laboratories category.
Summary
Combed and carded differ in fiber preparation, ring and open-end in spinning system; that is why combinations such as carded ring, combed ring and carded open-end exist. Combed yarn is more even, softer and less hairy than carded yarn; open-end yarn is more even, less hairy and cheaper than ring yarn, but weaker and harsher in handle with the same fiber. Which one is right depends on count, fabric, budget and specification together. You can find yarn suppliers in the cotton yarn category.
Frequently asked questions
What is the difference between combed and carded yarn?
The difference is whether the cotton is combed before spinning. Combed yarn (penye in Turkish) is spun from cotton that has been combed after carding; combing removes short fibers, neps and small trash. Carded yarn skips this step. According to Cotton Incorporated, combed yarn is more even, softer, stronger and less hairy, and suits finer counts; the price is a higher processing cost.
Is combed yarn the same as ring yarn?
No. Combed describes fiber preparation, ring describes the method of twisting the yarn. Cotton Incorporated writes that combed fibers are mainly used in ring yarn, but rotor (open-end) spinning with combed sliver has also been studied (Rowe, 1993). Write the two separately on a quote.
How much weaker is open-end yarn than ring yarn?
Cotton Incorporated writes that open-end yarn is 10–30% weaker than ring yarn from the same fiber, and gives 15–20% in another publication. The gap grows with long fiber and shrinks as fiber gets shorter; at some coarse counts open-end can even be slightly stronger. The result depends on fiber, count and machine settings.
Combed, carded or open-end yarn for a T-shirt?
The sources give no binding table matching count to product. Cotton Incorporated writes that ring yarn is used in lightweight fabrics and open-end yarn in underwear, socks, sweaters and outerwear; in Rieter's rotor example, T-shirt yarn is Ne 20–30 in 100% cotton. Tekstil Rehberi's starting point: if a fine, soft handle is the priority, ask for combed ring; if cost is the priority, ask for carded or open-end quotes too, and decide on a sample of the target fabric.
How much more expensive is combed yarn than carded yarn?
The sources do not give the size of the price gap. The reason is clear: combing is an extra step, it separates short fibers as waste (4–24% according to Cotton Incorporated, 8–25% according to NPTEL) and needs more machines and floor space. For a price, get a written quote from the supplier for the same count and the same preparation level.
How do you write the yarn type on a quote?
Write the fiber, fiber preparation, spinning system and count separately: “100% cotton, Ne 30/1, combed (penye) ring yarn”. Also state whether the combing is full or partial, and the evenness, yarn imperfection and hairiness values you require.
Sources (12)
- Cotton Incorporated, ISP 1006: Cotton Spun Yarns for Knit and Woven Fabrics, 2003 (pp. 1, 3–5, 7: yarn classes, process flow table, combing, ring and open-end comparison; accessed October 11, 2026)
- Cotton Incorporated (CottonWorks), Textile Yarns, approximately 2010 (pp. 7, 9–11, 13, 15–16, 19–21: carded and combed comparison, noil percentage, open-end, compact, vortex, count ranges; accessed October 11, 2026)
- Cotton Incorporated, TRI 1004: Introduction to Open-End Spinning, 2003 (pp. 3, 8–10: ring and open-end yarn formation, strength gap, hairiness; accessed October 11, 2026)
- NPTEL (IIT Delhi), short staple spinning course content: Combing, introductory chapter (accessed October 11, 2026)
- Rowe, T. (1993). Improvements in Rotor Yarn Quality When Using Combed Cotton Slivers. Proceedings of the 1993 Beltwide Cotton Conferences, National Cotton Council (abstract)
- Rieter, Spatafora, J. and Schwippl, H. (July 2020). Yüksek miktarda kısa elyaf içeriği için ideal open end iplikçilik prosesi (Ideal open-end spinning process for a high short-fiber content; title translated by us; Turkish edition), pp. 4–6: Uster Statistics curves, comber noil blends
- Rieter, Rotor Spinning Technology Kits and Components, R 40 – R 70 (manufacturer brochure, PDF file date March 2023; pp. 5, 7, 11, 13: denim, towel, T-shirt and sweatshirt application examples; accessed October 11, 2026)
- Candan, C., Nergis, U. B. and İridağ, Y. (2000). Performance of Open-End and Ring Spun Yarns in Weft Knitted Fabrics. Textile Research Journal, 70(2), 177–181 (abstract)
- Hailemariam, A. F. and Muhammed, N. (2024). Effect of ring and rotor spun yarns on denim fabric properties. Research Journal of Textile and Apparel, 28(1), 16–27 (abstract)
- TÜRKPATENT (Turkish Patent and Trademark Office), Bursa Havlusu (Bursa Towel) geographical indication registration, No. 1519, registered January 9, 2024 (Table 1 and production method; in Turkish; accessed October 11, 2026)
- ITMF, International Textile Industry Statistics, Vol. 66/2023, December 2024 (Tables 1.1 and 1.5; figures are estimates; copy hosted on the AITPA site; accessed October 11, 2026)
- Textile World (June 23, 2023). ITMF: Shipments of New Textile Machinery Decreased in Most Segments in 2022 Except in Spinning (report on ITMF shipment statistics; accessed October 11, 2026)
Author and fact-checking
Written by
Yarn and Spinning Editor
Murat Yıldız is Tekstil Rehberi's yarn and spinning editor. He covers yarn types, yarn count systems (Ne, Nm, Tex, denier), spinning technologies and the yarn market, and checks count conversions and yarn quality values against standards and manufacturer data.
Content by Murat YıldızFact-checked by: Gizem Polat
This content was prepared by the Tekstil Rehberi editorial team. Before publication, our verification editor checked its figures, dates and sources against primary sources.
Spotted an error? Email us at [email protected] How we work →
Related articles
Yarn Count Conversion: Ne, Nm, Tex and Denier Formulas and Tables
Conversion formulas and a table for Ne, Nm, tex and denier, how to calculate yarn count from a measurement, how to read plied counts such as 30/2, and the count mistakes that most often cause trouble in supplier orders.
Textile Trade Fairs 2026-2027: Istanbul and Europe Calendar
Dates, venues and focus of the main textile fairs in Istanbul and Europe from November 2026 to September 2027, which fair suits which buyer, and what to check before you travel.
Turkey Textile and Apparel Exports 2025: Markets, Products
Turkey exported US$16.77 billion of apparel and US$9.41 billion of yarn, fabric and fiber in 2025. See the top markets and products, and why official sources report different totals.